Postion: Home > Our Case > Stamping & Bending >
A dimension can pass inspection while the component still has the wrong burr direction, unstable springback, an unsuitable coating or a surface that does not make reliable contact.
Our review connects your drawing to the way the part will fit, carry load, conduct, protect or fasten in the finished product.
Email: info@hms1688.com
Send Drawing for Mobile QuoteSend PDF, STEP/STP, material, thickness and quantity. Drawing attachments can be emailed separately after submitting the form.
These questions help turn a general drawing into a practical stamping and inspection plan.
Identify datums, mating holes, slots, flange positions and the surfaces that actually control assembly.
Grade, temper, thickness, grain direction and inside radius can change cracking and springback behavior.
Burr direction and edge condition may affect insertion, wiring, operator handling or a nearby seal.
Grounding, conductive contact, threads and close fits may need coating masks or controlled build-up.
Welding, heat treatment, plating and assembly can alter geometry or appearance after the stamping operation.
Quick drawing check: If a dimension affects fit, sealing, electrical contact or load transfer, mark it clearly. General dimensions do not always need the same tolerance or inspection frequency.
Separate blanking, piercing or forming operations provide flexibility for selected simpler parts.
Review when: volume is moderate, geometry is straightforward or the project may still change.A strip moves through several stations so cutting and forming steps can run in sequence.
Review when: repeat volume can justify dedicated tooling and stable material feed.Material flows into cup-like or enclosed shapes through one or more drawing stages.
Review when: depth, radii, wall thinning, wrinkling and surface marks are important.Laser cutting, CNC bending, welding, machining, finishing or assembly can complete features not suited to the stamping tool.
Review when: the finished component combines formed details with inserts, welds or machined interfaces.Confirm critical interfaces, material, finish, quantity and how the part is used in the assembly.
Evaluate stamping method, station sequence, tooling access and necessary secondary operations.
Inspect agreed dimensions, form, burr and appearance against the approved drawing.
Use suitable in-process checks for the features that could drift with setup, feed or tooling wear.
Link repeat orders to the latest drawing revision, tooling version and relevant process notes.
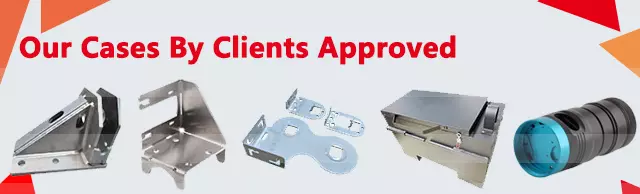
Contacts, battery brackets, covers and cabinet components.
Shields, connector supports, housings and internal frames.
Sensor brackets, clips, guards and mounting components.
Retainers, formed brackets, shields and support parts.
We can manufacture and inspect components to the approved drawing and agreed inspection scope. Overall load, fatigue, electrical, thermal, corrosion and regulatory validation should be defined by the customer or system integrator unless a separate scope is agreed.
No. Tolerance should reflect function, the datum strategy and the forming process. Identifying critical dimensions helps concentrate control and inspection on the features that affect assembly.
Sometimes, especially when geometry can be formed from sheet and expected volume supports tooling. Wall thickness, radii, holes, datums and secondary features need to be reviewed first.
A coating adds thickness and may collect differently around holes, threads or edges. Masking and post-finish dimensional requirements should be stated on the drawing.
The new revision should be compared with the existing tool. Some changes may use replaceable inserts or tool modification; others may require a different tooling route.
Send your drawing and identify the surfaces, dimensions or edges that control fit and function. We will review the stamping route before quotation.
Email: info@hms1688.com
Request Mobile Stamping ReviewDrawings, CAD files, samples and technical information are handled confidentially. NDA support is available for OEM projects.
Shenzhen Hongming Sheng Technology Co., Ltd. Tel\Wechat\Whatsapp:+86 18818409949
 Address: No. 132, Dongfa Road, Dongkeng Village, Gongming Street, Guangming New District, Shenzhen
 E-MAIL: info@hms1688.com

Copyright©2010-2026 Power by Jim design
 TOP